Precision Injection Mold Steel Selection & Tooling Guide
Engineered by Ningbo Mude Molding Technology Co., Ltd. Optimize cycle life, corrosion resistance, and polishability with certified steel grades. We tailor core and cavity steel solutions for custom precision injection molds, automotive exteriors, interior assemblies, and optical-grade components—systematically matched to resin abrasiveness, SPI Class 101 mold life standards, and Class-A surface finish requirements.
Mold Life Assurance
1,000,000+ Cycles
SPI Class 101 production longevity
Material Traceability
100% Genuine MTR
Original mill inspection certificates
Machining Precision
±0.01 mm Accuracy
5-axis high-speed CNC & CMM verified
Alloy Versatility
Pre-Hard to CuBe
S136, 718H, NAK80 & thermal alloys
Injection Mold Steel Selection: 4 Core Engineering Decision Criteria
Ningbo Mude Molding Technology Co., Ltd applies systematic metallurgical principles to align steel grades, surface treatments, and thermal performance with target mold lifecycles and resin demands across high-durability injection molds.
The Four-Pillar Engineering Framework
Reliable mold performance starts with thorough resin evaluation, moldflow thermal modeling, and comprehensive DFM analysis before CNC cutting begins.
Resin Abrasiveness & Corrosiveness
Abrasive glass-filled engineering resins (PA-GF, PBT-GF) require wear-resistant H13 or SKD61, while corrosive PVC and flame-retardant resins demand high-chromium stainless steel (S136, 1.2083).
SPI Surface Finish & Texture Specs
High-gloss automotive components and optical light guides mandate ESR remelted steels (NAK80, S136 ESR) to eliminate inclusions, ensure SPI A-1 mirror polishing, and accept uniform Mold-Tech etching.
Production Volume & SPI Mold Class
SPI Class 101 production molds (1,000,000+ shots) require vacuum through-hardened alloys at 48–52 HRC, whereas Class 103 mid-volume programs optimize economics using pre-hardened P20 or 718H.
Thermal Conductivity & Cycle Optimization
Deep core ribs, bosses, and hot-runner gates integrate high-conductivity beryllium copper (BeCu) or Ampcoloy inserts to dissipate heat rapidly, eliminating sink marks and cutting cycle times by 15%–30%.

Quality assurance includes 100% original mill test certificates (MTR), ultrasonic non-destructive flaw detection, and multi-point calibrated Rockwell hardness verification on all core and cavity inserts.
Standard Steel Grade Comparison Matrix
Technical specifications engineered to match polymer chemistry, tooling hardness requirements, and target production lifecycles.
| Steel Grade | Delivery State | Hardness (HRC) | Corrosion Resistance | Polishability (SPI) | Target Shot Life |
|---|---|---|---|---|---|
| P20 / 1.2311 | Pre-hardened | 28 - 32 | Standard | SPI B-2 | 100K - 300K |
| 718H / 1.2738 | Pre-hardened Modified | 33 - 38 | Moderate | SPI B-1 | 300K - 500K |
| NAK80 | Pre-hardened Age-treated | 37 - 43 | Moderate | SPI A-2 | 500K - 800K |
| S136 / 1.2083 ESR | Through-hardened (Quenched) | 48 - 52 | Superior (High-Cr Stainless) | SPI A-1 (Mirror) | 1,000,000 |
| H13 / 1.2344 ESR | Vacuum Through-hardened | 48 - 54 | Good | SPI A-2 | 1,000,000 |
ESR Micro-Purity Control
We specify vacuum degassing and electroslag remelting (ESR) to eliminate non-metallic inclusions, preventing pitting and micro-cracking across high-gloss automotive surfaces.
Vacuum Heat Treatment
Multi-stage computer-controlled quenching and deep sub-zero cryogenic tempering eliminate internal stresses and retained austenite, holding dimensional accuracy within ±0.01 mm.
PVD & Nitride Surface Engineering
Advanced DLC, CrN, and gas ion nitriding processes boost surface hardness to 65–70 HRC, cutting demolding drag and extending wear life on high-friction lifters and slides.
Injection Mold Steel Grades: Technical Properties & Performance Matrix
Ningbo Mude Molding Technology Co., Ltd matches tool steels directly to resin corrosiveness, filler abrasiveness, optical clarity requirements, and SPI mold class life cycles. Review our cross-reference chart covering international standards (AISI, DIN, JIS), heat-treated hardness, and automotive component suitability.
| Standard Grade (AISI / DIN / JIS) | Delivered Hardness | Polishability Rating | Wear Resistance | Corrosion Resistance | Target Production Volume |
|---|---|---|---|---|---|
| P20+S / 1.2312 / SCr440 | 28–34 HRC (Pre-hardened) | SPI B2 (Standard Technical) | Moderate | Basic (Oil-Protected) | Up to 300,000 Shots (SPI Class 103) |
| 718H / 1.2738 / HPM-7 | 33–38 HRC (Pre-hardened) | SPI B1 to SPI A3 | Moderate to High | Standard | 500,000+ Shots (Automotive Fascias) |
| NAK80 / Precipitation Hardened / NAK80 | 37–43 HRC (Uniform Core) | SPI A1 (Ultra-High Gloss) | High (EDM Stable) | Standard | 500,000 to 800,000 Shots |
| S136 / 1.2083 ESR / SUS420J2 | 48–54 HRC (Vacuum Quenched) | SPI A1 (Optical Mirror Finish) | Exceptional | Superior (Acid & Rust Proof) | 1,000,000+ Shots (SPI Class 101) |
| H13 / 1.2344 ESR / SKD61 | 46–52 HRC (Through-Hardened) | SPI A2 (Precision Spec) | Superior (Thermal Fatigue Resistant) | Moderate | 1,000,000+ Shots (GF-Reinforced) |
| D2 / 1.2379 / SKD11 | 58–62 HRC (Deep Quenched) | SPI C1 (Functional Grind) | Maximum (Severe Abrasion) | Moderate | Lifter & Gate Core Inserts |
Certified Mill Origin & Defect-Free Metallurgical Integrity
Substandard steel cores trigger cavity sink, stress fractures, and unexpected production halts. Mude Molding procures authentic forged blocks directly from premier mills including ASSAB, Daido, and Kind&Co, verifying chemical composition and micro-cleanliness prior to 5-axis CNC machining.
Class A internal soundness checks eliminate hidden voids and porosity.
Multi-zone Rockwell testing guarantees uniform temper across heavy blocks.

Corrosive Resin Tooling
Resins like PVC, POM, and halogenated flame-retardants release acidic vapors during plastification. We specify vacuum electroslag-remelted S136 or 1.2083 ESR stainless steel to prevent mold pitting and sustain polished shut-off surfaces.
Glass-Filled & Abrasive Resins
Compounds loaded with 30% to 50% glass fiber cause rapid gate erosion and parting-line flash. Through-hardened H13 (1.2344) or D2 inserts deliver exceptional carbide hardness to protect tight automotive tolerances over long runs.
High-Gloss & Optical Parts
Automotive lighting lenses, light guides, and piano-black trims require zero microscopic inclusions. Vacuum-degassed NAK80 and S136 ESR permit diamond paste buffing to an SPI A-1 mirror standard without orange peel or pitting.
Critical Core and Cavity Inserts with Advanced Thermal Alloys
Ningbo Mude Molding Technology Co., Ltd. engineers precision tooling inserts pairing hardened tool steels with high-conductivity copper alloys. We optimize thermal balance across complex automotive, appliance, and electronic part geometries—slashing cycle times by 15% to 30%, preventing sink marks and warpage, and eliminating slide galling.
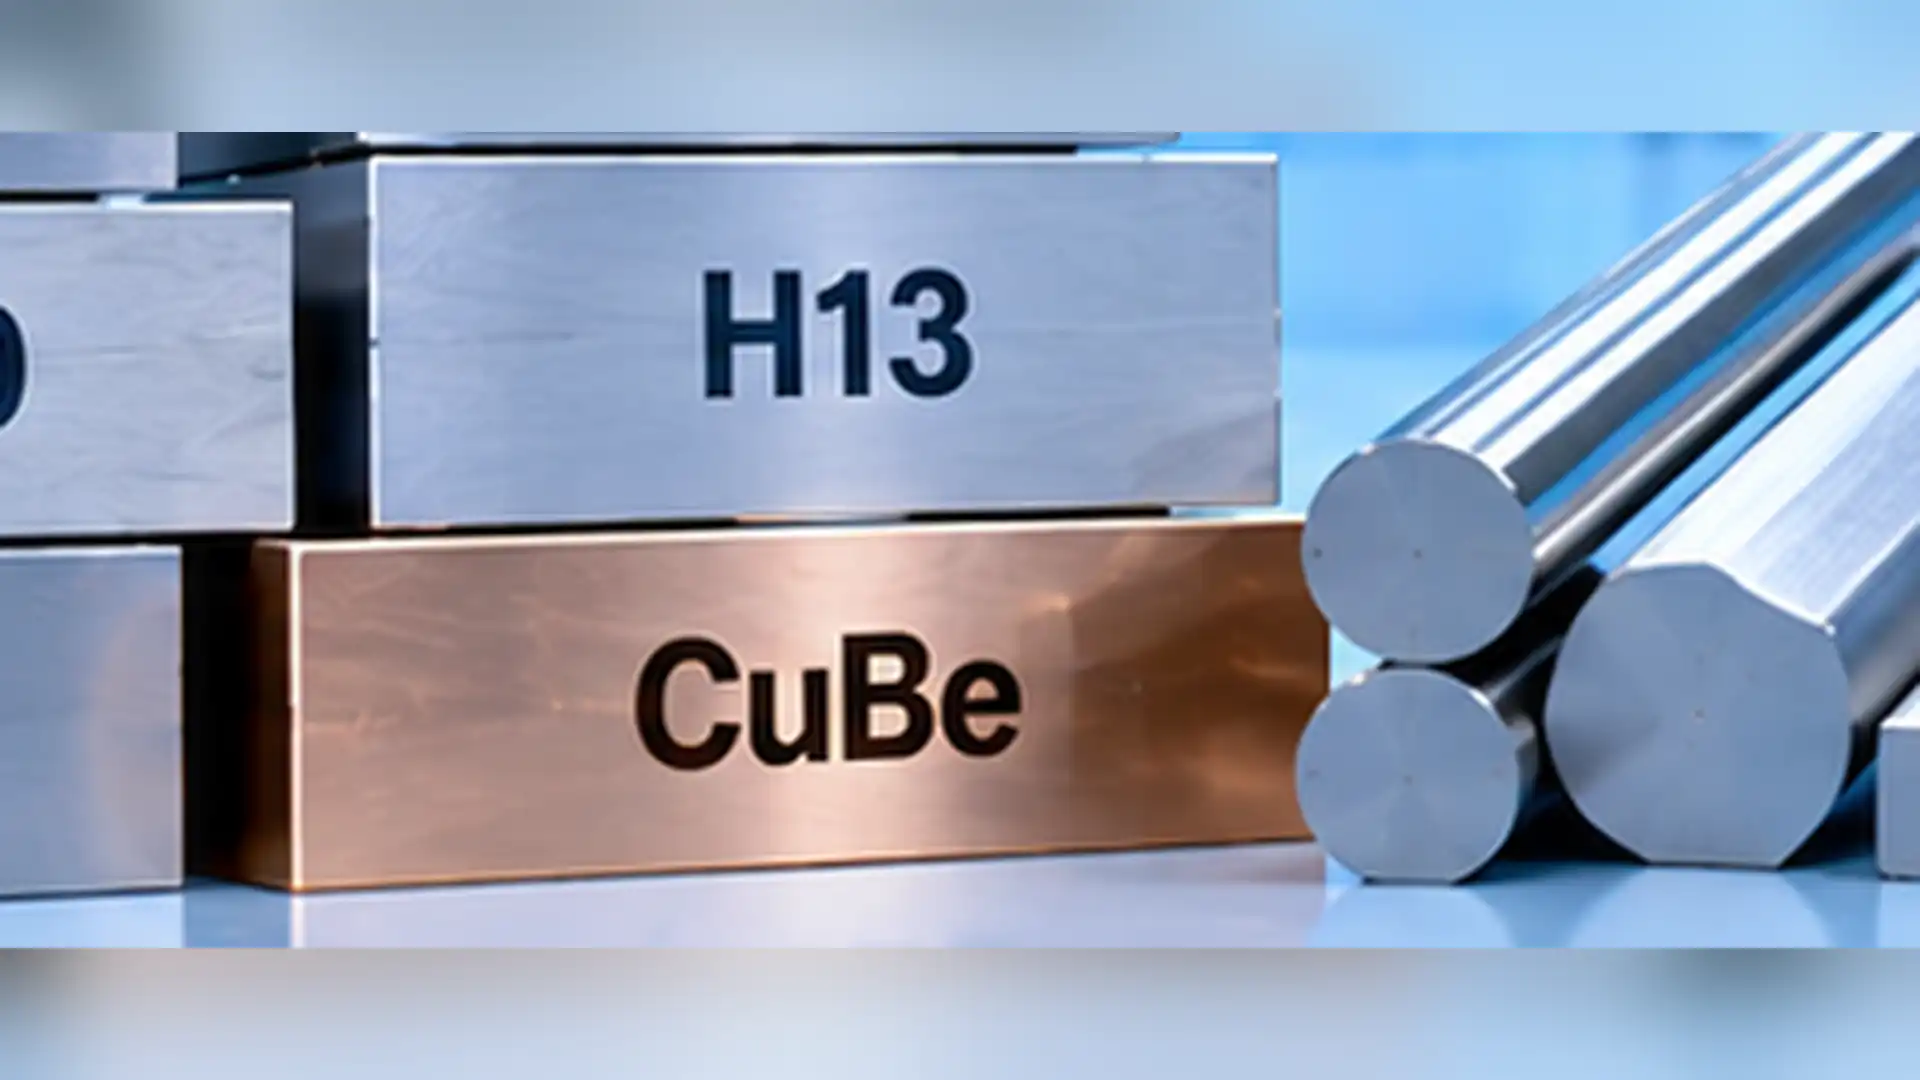
Targeted Thermal Extraction in Hard-to-Cool Features
Deep ribs, tall bosses, and perimeter gates trap intense heat that standard drilled waterlines cannot reach. By embedding Beryllium Copper (MoldMAX) and Ampcoloy inserts, thermal energy transfers up to 5 times faster than conventional mold steels, stabilizing temperature fields and eliminating localized shrink defects.
Beryllium Copper & Ampcoloy Thermal Alloys
Delivering thermal conductivity up to 130–240 W/(m·K), our premium copper alloy inserts extract heat rapidly from deep automotive grille fins, thick mounting bosses, and tight pin clusters.
Anti-Galling Slides, Lifters & Wear Components
Dynamic actions, angle lifters, and side-action cores utilize vacuum-hardened SKD61 or H13 (HRC 50–54) with ion nitriding, matched against self-lubricating graphite bronze plates to eliminate metal pickup.
Hybrid Conformal Cooling & Sub-Insert Integration
We integrate DMLS 3D-printed stainless steel conformal cooling cores with precision-ground pocket inserts, achieving uniform cooling curves across contoured class-A automotive exterior panels.
Faster Heat Extraction
Copper alloy inserts draw trapped thermal energy away from thick ribs and gates, preventing localized sink marks and plastic degradation.
Shorter Cooling Time
Targeted cooling inserts cut mold cooling intervals significantly, accelerating per-hour production rates for complex automotive assemblies.
Nitrided Wear Surfaces
Ion-nitrided SKD61 lifter bodies and PVD-coated slides endure long-run friction, ensuring SPI Class 101 longevity beyond 1,000,000 cycles.
Pocket Interfacing Tolerance
High-speed 5-axis CNC and mirror wire-EDM guarantee seamless insert alignment, zero parting-line witness marks, and leak-free O-ring sealing.
Thermal Treatment & Advanced Surface Modification Technologies
Ningbo Mude Molding Technology Co., Ltd integrates controlled vacuum heat treatment, sub-zero stabilization, and thin-film PVD coatings to eliminate distortion, resist abrasive resin wear, and secure SPI Class 101 mold life.

Programmable multi-stage preheating and inert gas quenching protect core geometries within ±0.01 mm tolerances, eliminating post-quench micro-cracking and EDM stress build-up.
Low-temperature ion nitriding establishes a resilient diffusion zone that eliminates galling on automotive sliders, lifters, and high-frequency parting shut-offs.
Combining through-hardened alloy matrices with anti-wear barrier coatings delivers sustained fatigue resistance against 30%+ glass-fiber filled and corrosive polymer grades.
Core Metallurgical & Finishing Capabilities
Systematic post-machining hardening regimes engineered for automotive exterior tooling, optical lenses, and high-wear engineering polymers.
Vacuum Quenching & Tempering
Oxygen-free atmosphere prevents decarburization and scale on high-alloy tool steels like S136, H13, and 1.2344 ESR, ensuring uniform through-hardening for high-impact molds.
Gas & Ion Plasma Nitriding
Precision thermochemical nitrogen diffusion creates an ultra-hard sliding layer without thermal deformation, ideal for automotive grille sliders, angle pins, and ejector systems.
PVD & DLC Hard Coatings
Nanostructured DLC, CrN, and TiN coatings dramatically lower friction coefficients, preventing demolding scuffs and shielding cavities against corrosive flame-retardant outgassing.
Cryogenic Deep Freeze Treatment
Liquid nitrogen sub-zero cycles convert unstable retained austenite into uniform martensite, locking in micro-dimensional stability across optical light guides and lens molds.
Heat Treatment & Surface Metallurgy Specification Matrix
Validated metallurgy standards applied across automotive exterior, interior, and precision electronic tooling programs at Mude Molding.
| Treatment Process | Compatible Steel Grades | Target Hardness / Depth | Core Engineering Benefit | Verification Protocol |
|---|---|---|---|---|
| Vacuum Quenching & Triple Tempering | S136, H13 (1.2344 ESR), SKD61, 420ESR | 48 – 54 HRC (Through-Core) | High core toughness, zero decarburization, SPI A-1 polishability | ASTM E18 / ISO 6508 (Multi-Point) |
| Controlled Gas / Ion Nitriding | 718H, 1.2738HH, P20+Ni, SKD61 | 900 – 1100 HV (0.10 – 0.25 mm) | Anti-scuffing for large sliders, angle lifters, and wear plates | DIN 50190-3 / Micro-Vickers |
| Functional PVD Coating (DLC / CrN) | Quenched S136, H13, Pre-hardened Tool Steels | 2.0 – 4.0 µm Film Thickness | Resists 30%+ GF polymer abrasion and eliminates drag marks | ASTM C1624 Scratch & Adhesion Test |
| Cryogenic Deep Freeze (-196°C) | S136-SUP, NAK80, 1.2083 ESR, DC53 | < 0.5% Retained Austenite | Eliminates dimensional drift on optical reflectors and high-gloss molds | X-Ray Diffraction (XRD) Phase Analysis |
Custom Tool Steel Solutions for Automotive Interior & Exterior Systems
Ningbo Mude Molding Technology Co., Ltd matches premium metallurgical compositions to Tier-1 injection molding performance and surface finish requirements.
Engineered Steel Pairings for High-Volume Vehicle Production
Production programs for high-volume exterior components and automotive interior accessories demand targeted mold steel selection. We balance core machinability, polishing purity, texture uniformity, and abrasive resistance to optimize production cycles and extend tooling life across demanding vehicle programs.
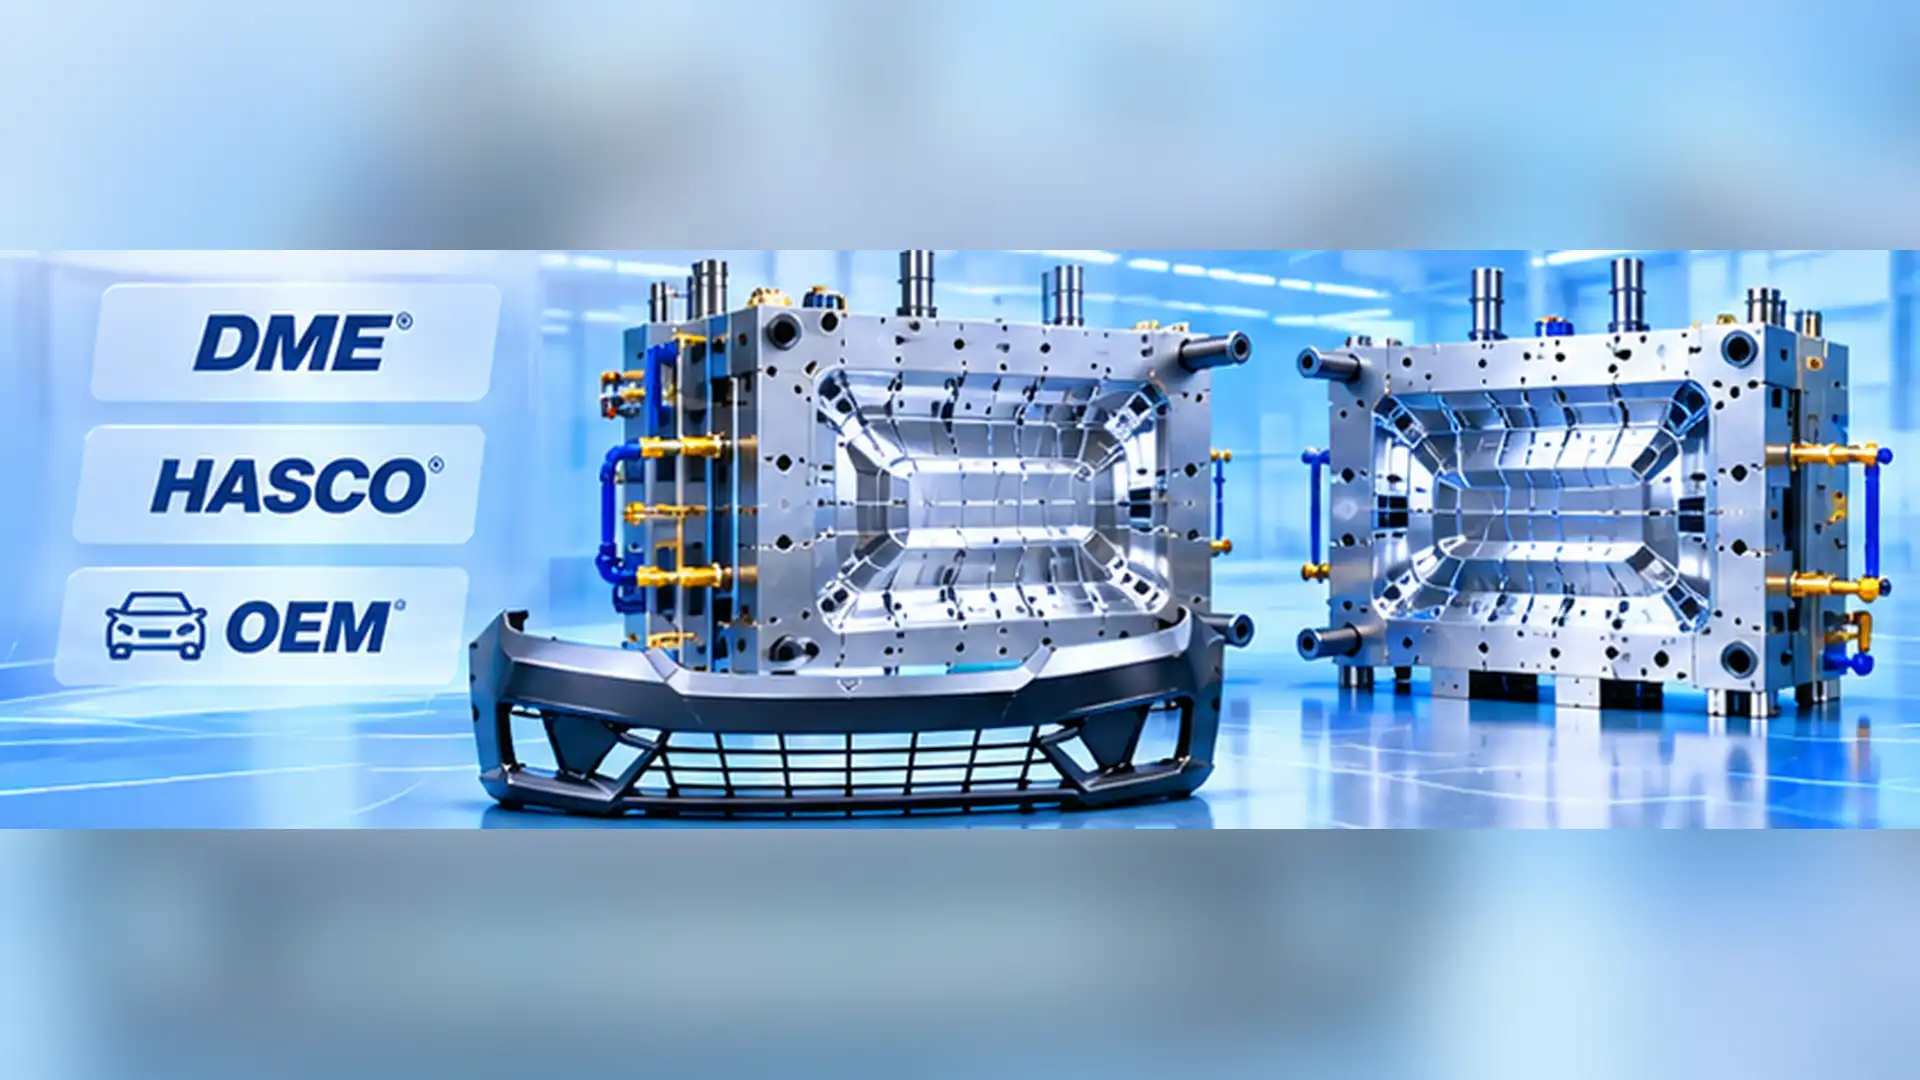
Large Exterior Parts
Bumpers, fascias, and spoilers require high core toughness, stable EDM performance, and uniform grain response across wide surfaces.
High-Gloss & Plated Grilles
Piano-black trims and electroplated front grilles mandate vacuum-remelted ESR steels to eliminate pinholes and surface inclusions.
Precision Interior Modules
Instrument panels, door trims, and pillar assemblies demand pre-hardened steels optimized for Mold-Tech texturing and dimensional stability.
Optical Lighting Modules
PC/PMMA headlamp lenses and light guides require corrosion-resistant stainless steel capable of SPI A-1 diamond mirror polishing.
Automotive Injection Tooling Material Specification Matrix
Standardized material guidelines engineered and verified by Ningbo Mude Molding Technology Co., Ltd.
| Application Domain | Critical Components | Primary Operational Stress | Matched Steel Grade | Hardness (HRC) |
|---|---|---|---|---|
| Large Exterior Aerodynamics | Front Bumpers, Rear Fascias, Spoilers | Core-cavity thermal balance & large-span dimensional stability | 718H / DIN 1.2738HH | 34 - 38 HRC |
| High-Gloss & Electroplated | Radiator Grilles, Pillar Appliques, Emblems | Pinhole defects, high injection pressure & mirror wear | S136 ESR / 1.2083 ESR | 48 - 52 HRC |
| Textured Interior Systems | Instrument Panels, Door Trims, Center Consoles | Uniform photo-etching, grain clarity & weld line mitigation | NAK80 / 1.2738 / P20+Ni | 36 - 40 HRC |
| Optical & Transparent Parts | Headlamp Lenses, Light Guides, DRL Optics | Polymer gas corrosion, haze, & SPI A-1 optical finishing | S136-SUP / 420 ESR | 50 - 54 HRC |
100% Mill-Certified Tool Steel & Rigorous Incoming Inspection
Ningbo Mude Molding Technology safeguards automotive tooling life through comprehensive quality-control protocols, multi-stage metallurgical verification, ultrasonic flaw screening, and full heat-lot serialization before any block enters machining.
Original Mill Test Certification (EN 10204 3.1)
Every mold base, cavity plate, and core insert arrives with genuine mill certificates from top producers (ASSAB, Daido, Kind&Co, Groeditz), guaranteeing chemical purity and eliminating counterfeit steel risks.
Ultrasonic NDT & Spectrometric Chemistry Verification
Incoming tool steel undergoes 100% ultrasonic non-destructive testing to detect internal voids and porosity, followed by optical spectrometry to confirm precise Cr, Ni, Mo, and V alloying compositions.
Through-Hardness Profiling & ERP Batch Serialization
Multi-point surface and core hardness testing verifies uniform quench-and-temper values (HRC), while unique ERP serial codes bind each raw block directly to tooling drawings and CMM inspection dossiers.

Rigid Non-Conforming Material Quarantine
All raw stock is locked electronically and physically upon arrival. Tooling blocks are released to CNC programming only after ultrasonic, hardness, and chemical assays confirm full compliance with SPI standards.
Complete furnace heat-lot verification for all cavity and core inserts.
Full ultrasonic NDT screening eliminates hidden inclusions and fractures.
Comprehensive mapping ensures consistent wear resistance throughout blocks.
Uninspected feedstocks never enter our CNC machining or EDM lines.
Injection Mold Steel Selection & Tooling Materials FAQ
Review technical guidelines on metallurgical grades, vacuum heat treatments, cycle time thermal optimization, and raw material traceability protocols from Ningbo Mude Molding Technology Co., Ltd.
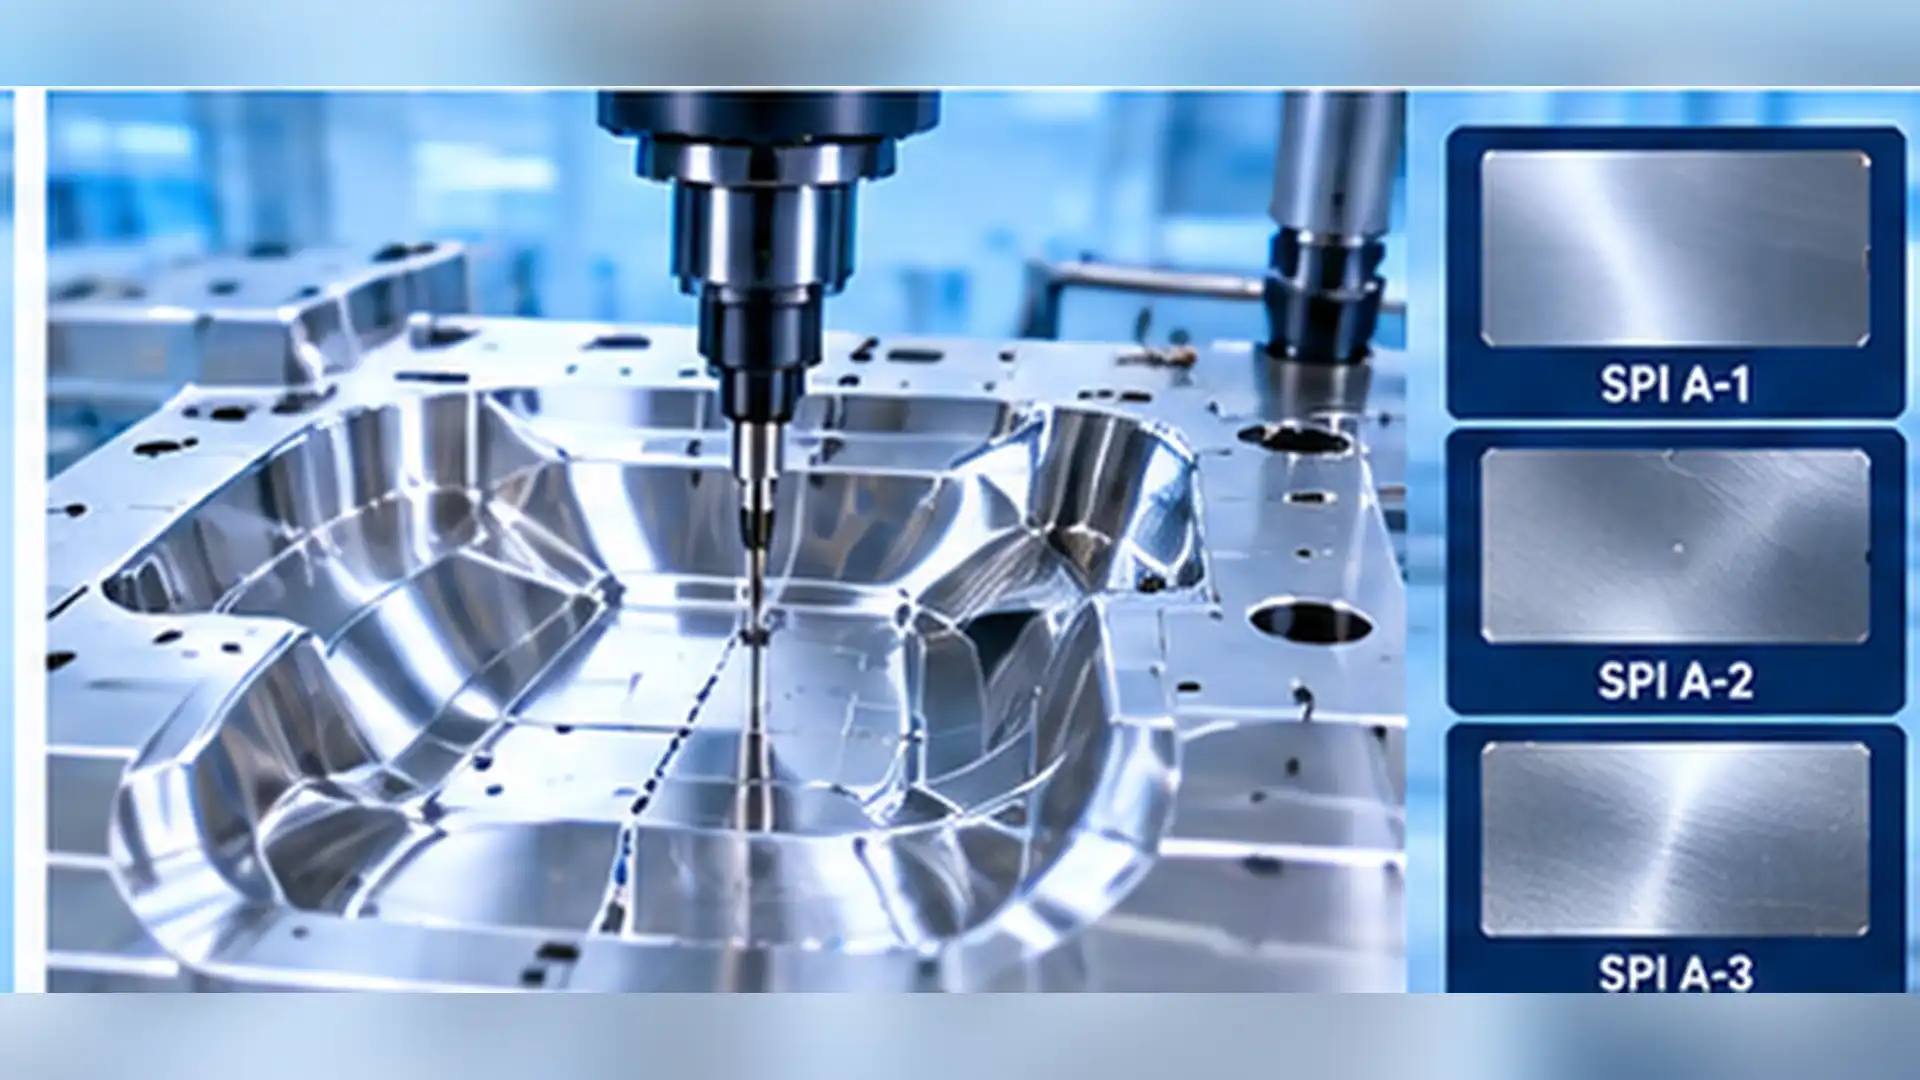
Tooling Steel Feasibility & DFM Review
Our design and engineering team conducts full Moldflow simulations and resin-specific metallurgical reviews prior to rough milling, balancing tool life, cycle efficiency, and upfront tooling capital.
Need a Custom Steel Recommendation?
Submit your 3D CAD models and production forecasts for an engineer-led steel grade evaluation, thermal heat sink assessment, and gate erosion mitigation analysis.